
Quality
Built on recognized standards.
Our quality systems are documented, audited and maintained so that every product we make can be traced back to the standard it was built against.
- Audited quality management systems
- Supplier qualification program
- Regulatory registrations and facility listings
- Raw-material identity and purity controls
- Documented batch records and full traceability
- Written SOPs across every process step



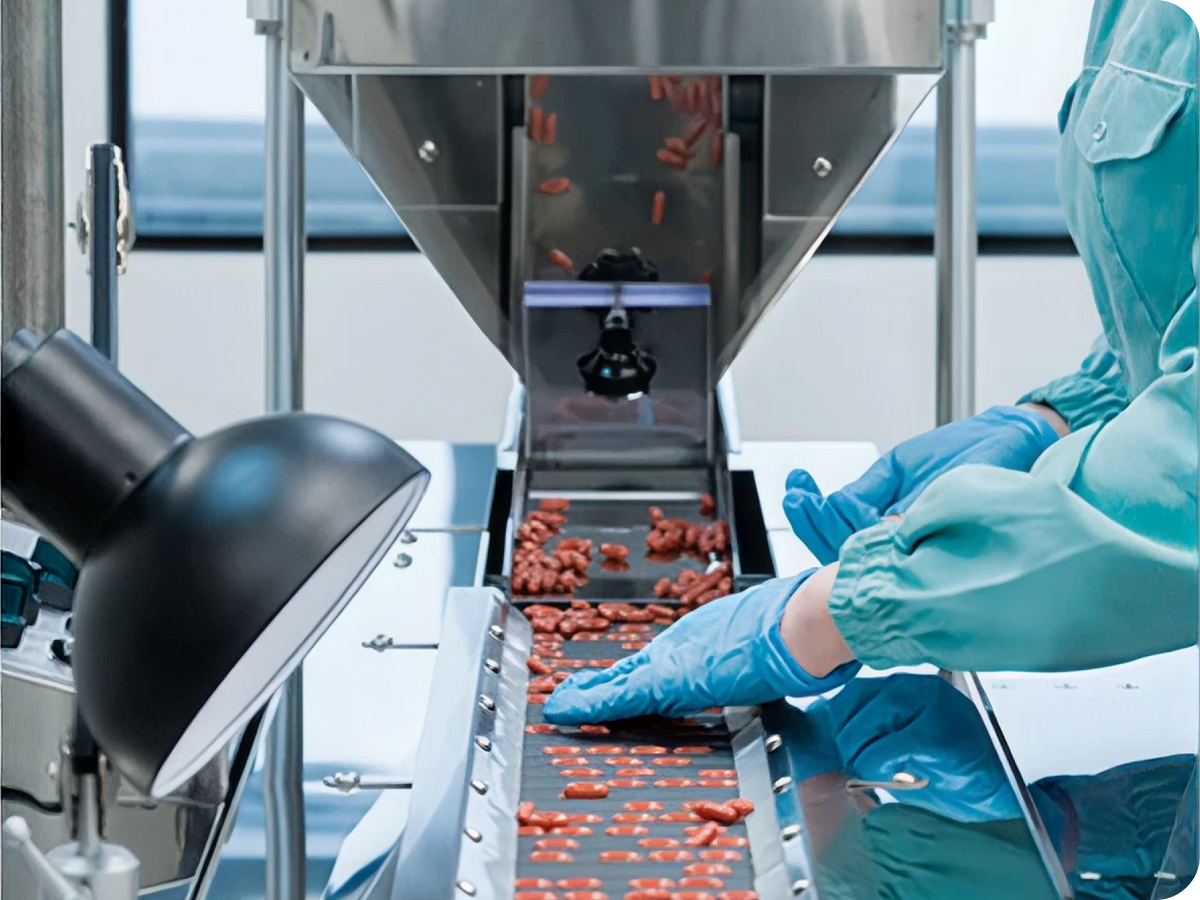
Precision at every stage.
From first formulation to the finished, labeled pack, production runs under one roof — which keeps timelines short, handoffs few and quality visible end to end.
- Formulation and product development
- Powders, capsules, tablets and sachets
- Blending, encapsulation and tableting
- Primary and secondary packaging
- Fast-melt and chewable delivery formats
- Private label and contract manufacturing
Tested for confidence.
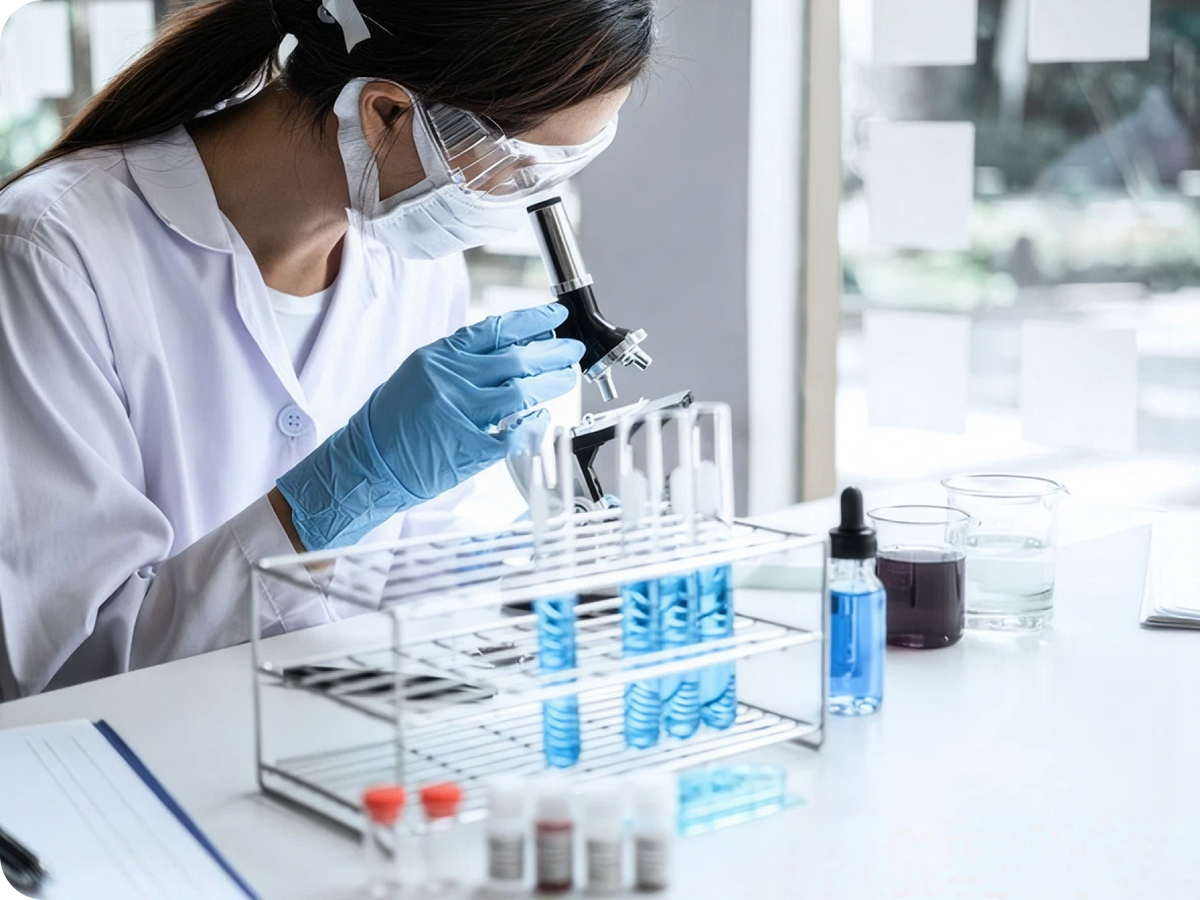
Nothing leaves the building on assumption. Material is checked on the way in, monitored through production and tested again before release.
- Raw-material identity and purity checks
- Stability and shelf-life programs
- In-process quality checks at every stage
- Finished-product release testing
- Analytical and microbiological testing
- Retained samples and test documentation
Designed for quality.
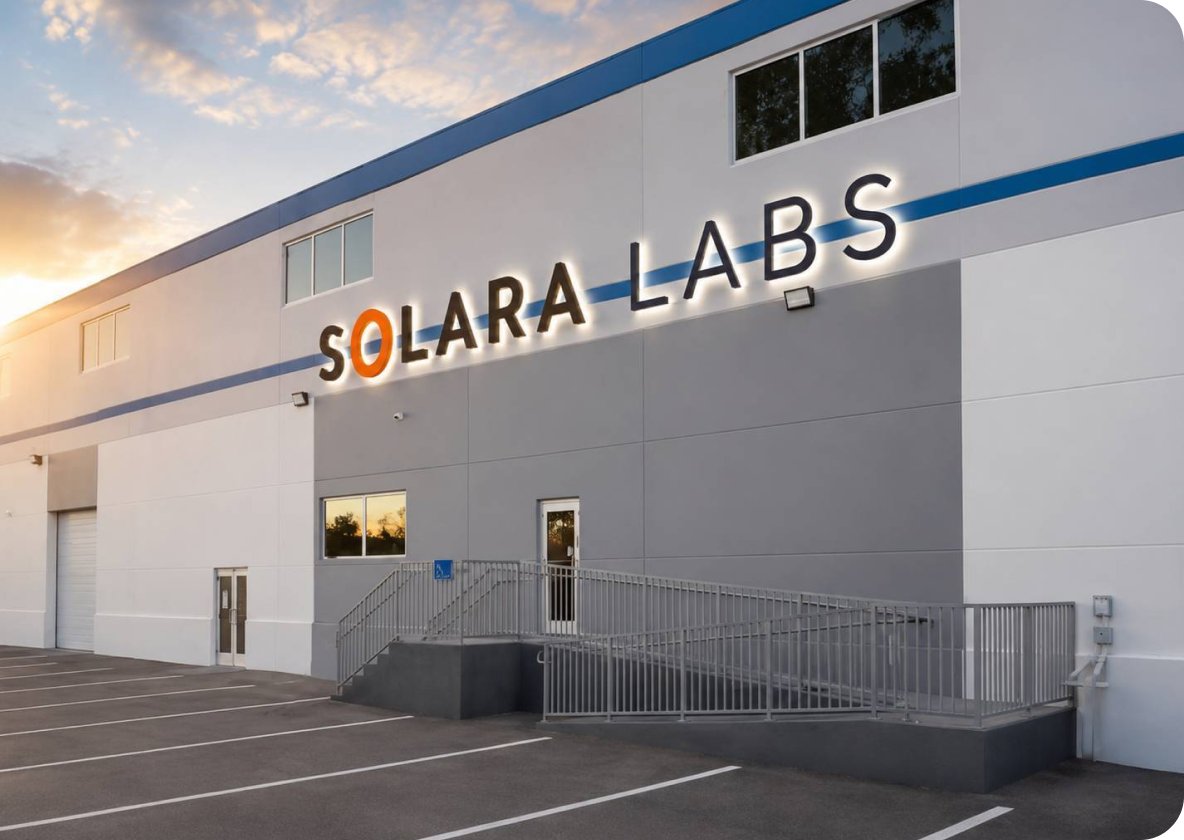
A purpose-built site in Florida where formulation, production, laboratory and packaging sit alongside one another — so oversight is direct rather than outsourced.
- FDA-registered production site
- On-site QC laboratory
- Controlled manufacturing environments
- Warehousing and distribution
- Modern production and packaging lines
- Capacity to scale with demand

Manufacturing Services
Building a brand of your own?
Solara offers contract development and manufacturing for select partners. Our science-led team can take you from formulation through finished product.